
Why are support materials necessary in 3D printing, and how are they removed?
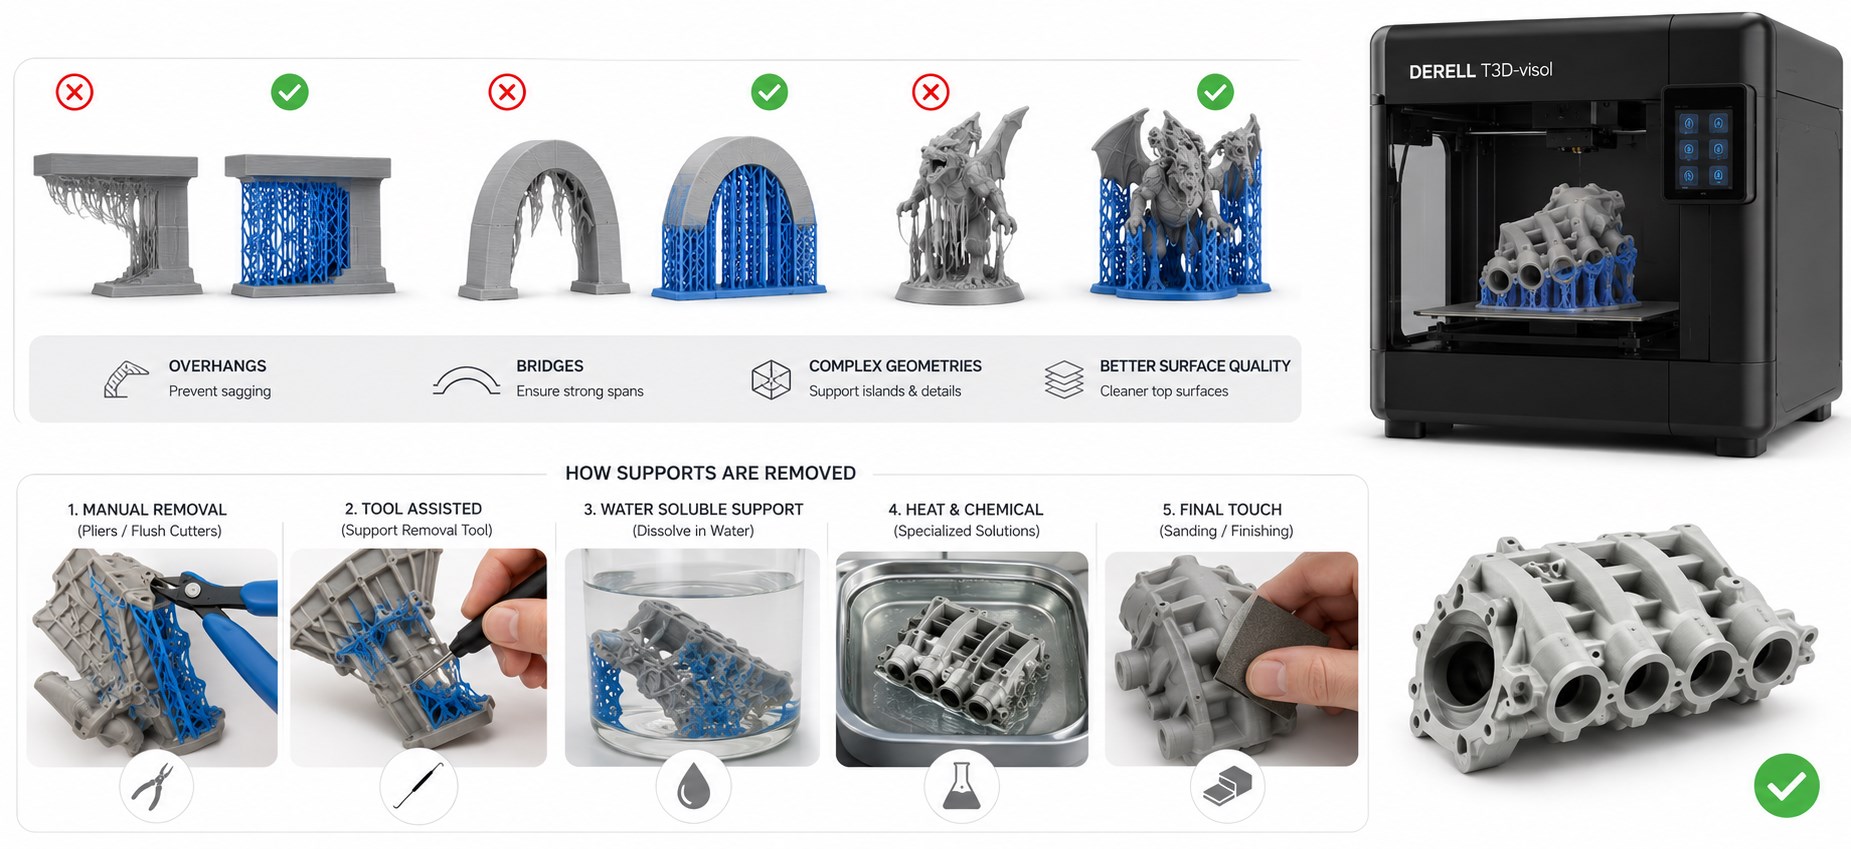
Plan how supports hold the print and how they will come off
In 3D printing, a support is a temporary structure that carries or anchors particular regions during production. It can prevent sagging, connect a newly formed region to the part and, in some metal processes, transfer heat to the build platform. However, support requirements, materials and removal methods depend on the printing technology. Good support design considers both successful printing and cleaning the part without damage.
Editor's note: Infill and temporary supports are different structures. FFF/FDM infill is a planned internal structure that remains in the part and can support its top layers. Removable supports are intended to be taken out afterwards. Internal cavities do not all need to be filled with supports; inaccessible supports can obstruct usable space. Assess infill's effect on strength separately.
Distinguish overhangs, bridges and disconnected regions
In FFF/FDM, a new extrusion extending beyond the material below can sag. A bridge spans a gap between regions that support its ends; short bridges can print without supports when settings are suitable. A new region with no connection underneath is a different case. These geometries behave differently across printing technologies.
No single overhang angle or bridge length applies to every part. Material, extrusion width, cooling and speed affect the result. Check the plane from which your slicer measures the angle, then establish the limits of your own profile using a small test geometry. Avoid treating one angle as a universal printer rule.
Consider orientation and access before adding supports
Rotating the part, changing a slope or splitting and joining a suitable design can reduce support requirements. For complex geometries, consider visible faces, mating regions and access for removal tools together. Preserve a suitable loading direction relative to the layers when changing orientation; the position requiring the least support is not always the right one.
If a channel contains supports, identify their exit route during design. Soluble supports also require liquid access, removal of dissolved material and subsequent cleaning. A completely sealed cavity does not become cleanable simply by using soluble supports. Layer height and detail resolution also influence whether small channels can be produced successfully.
FFF/FDM contact gaps and interface settings matter
Assess top contact Z distance, XY separation, interface layers and support pattern together. Too little separation can fuse the support to the model; too much can allow the underside to sag. Organic or tree-like supports can reduce contact in some geometries, but are not the best choice for every model. Inspect the layer preview and avoid a universal gap setting. Start with a profile suited to the filament properties, using support enforcers or blockers where needed.
Keep removal forces away from delicate features
Supports printed in the model material can be separated in small sections after the part has cooled appropriately. Use pliers or flush cutters at accessible support connections, without levering against thin walls, small pins or hole edges. If a connection resists, inspect the cutting direction and remaining attachments before pulling harder.
Removing a large support block in one motion can tear material from the part. An inaccessible contact is a design problem to address before printing. Check critical dimensions and fits afterwards; a clean exterior does not demonstrate that all internal supports have been removed.
Separate breakaway materials from soluble supports
Compatible multi-material systems can print the model and supports using different materials. Breakaway supports are removed mechanically and require access. Suitable materials such as PVA dissolve in water. Check compatibility with the model material, printing temperatures, adhesion and the part's resistance to the bath conditions. Not every soluble support is removed using water alone.
Follow the manufacturer's storage and processing conditions. Where appropriate, mechanically reducing excess support first can reduce the dissolution load; avoid stressing delicate features. After dissolution, inspect channels and blind regions, and complete the required rinsing and drying. Soluble supports do not automatically provide a mark-free surface or eliminate labour.
Washing and cutting supports are separate steps in SLA, DLP and MSLA
In conventional resin processes, supports are generally solid structures made from the model resin. IPA washing removes liquid resin from the surface; it is not a general method for dissolving solid supports. Supports are separated mechanically at their contact points using suitable cutting tools.
Choose the washing, drying, required post-curing and support-removal sequence for the material. For example, Formlabs' general SLA guide recommends removing supports after post-curing to limit deformation; the resin-specific instructions take priority. Appropriate surface finishing can remove remaining contact marks. Excessive sanding can alter fine details or dimensions.
Assess material jetting processes such as PolyJet separately
Some PolyJet systems use gel-like supports distinct from the model material. Depending on the support and printer, removal can involve manual separation, water pressure in a suitable enclosed cleaning unit or a specified chemical process. Stratasys instructions distinguish methods by material code. Do not transfer a PolyJet cleaning method to conventional SLA resin. Water pressure can also damage delicate features.
Polymer SLS generally needs no separate support structures
In polymer SLS, unsintered powder surrounding the component provides a supporting environment during production. Separate solid supports of the kind used in FFF or SLA are generally unnecessary. Cooling, extracting parts from the powder and cleaning surfaces and internal channels remain necessary. Having no support structures does not mean having no post-processing. Do not generalise this behaviour to metal laser powder bed fusion.
Metal powder bed supports also help control heat and distortion
In metal PBF-LB, supports can anchor the part to the platform while providing heat paths and helping control distortion. These functions differ from loose powder surrounding a component. Reducing support material must preserve thermal stability and build reliability; in industrial production, the support strategy belongs in the process plan.
Stress-relief heat treatment is not a method that makes supports disappear. Follow a qualified sequence for heat treatment, separation from the build plate and support removal. Wire EDM, sawing, suitable hand tools or CNC machining may be used. Plate separation and removal of remaining supports can be distinct operations. Plan machining allowances and workholding for critical regions in advance.
Laser and ultrasonic methods are not universal solutions
Specialist equipment can assist support removal or cleaning. However, laser ablation and ultrasonic baths are not standard support-removal steps for every print. Ultrasonic agitation can assist a cleaning process without necessarily separating every solid support without damage. Use only a method approved for the combination of material, liquid and equipment.
Include final inspection and support costs
Inspect contact regions for cracks, tearing, pits and residue. Plan any required mechanical verification around the part after support removal and finishing. Connect relevant standards and acceptance requirements to the drawing, and use more than visual inspection for critical surfaces.
Total time and cost include removal, bath processing, drying and surface repair alongside printing the supports. In a hypothetical job using a 20 g model and 10 g of supports, those two items alone consume 30 g of material. A different orientation may reduce supports, but surface quality, strength and access need reassessment. Trial both printing and removal on a small sample before deciding.
The workspace and waste belong in the workflow
Cut support fragments can fly off; use suitable eye protection. Select ventilation and protective equipment according to the safety data sheet when handling resin, solvents or metal powders. Do not place flammable solvents in heaters or ultrasonic equipment without verified suitability. Dissolved support and washed-off resin remain in the bath; plan waste handling according to the material and process instructions.
Sources
Prusa: Interfaces, contact distances and support styles
Prusa: Bridging, test prints and orientation
UltiMaker: Model-material, PVA and Breakaway supports
Formlabs: SLA washing, drying, curing and support removal
Formlabs: Removing support contact marks
Stratasys: Cleaning methods for specific PolyJet supports
EOS: Polymer SLS without separate support structures
Materialise: Heat transfer and distortion control with metal supports
Protolabs: Distinguishing metal support removal from heat treatment